


Distribution mixers


Distribution mixers
The distribution mixer has its place upstream of the centrifugals, where it ensures a quick and even product feed. It homogenises the massecuite and creates defined feed conditions, thus making a substantial contribution to optimum capacity use, excellent separation in the centrifugals and a stable overall process.
Functions
In the distribution mixer, the sugar crystals are kept in continuous motion by an agitator. This prevents sedimentation, the formation of agglomerates and caking.
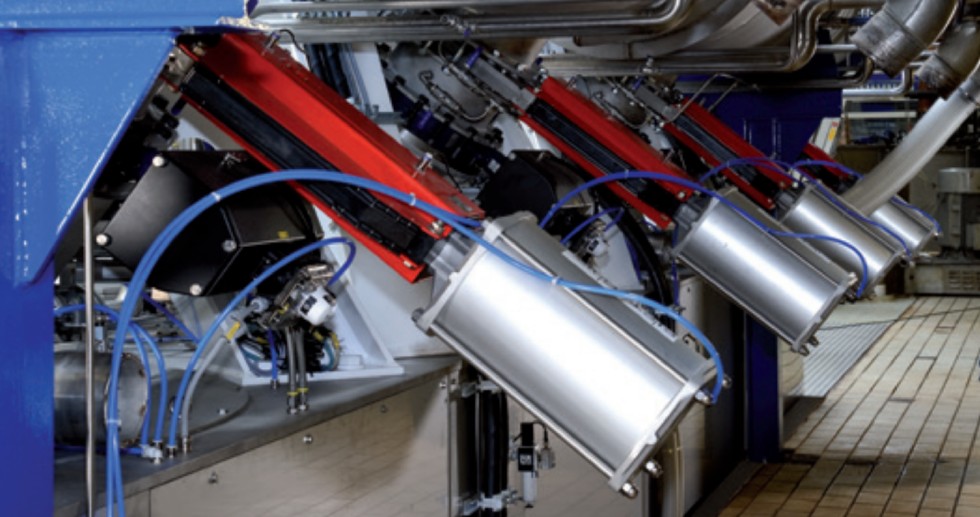
The distribution mixer permits quick and even filling of one or several centrifugals, which helps optimise centrifugal operation. If required, an optional dome will ensure sufficient and constant system pressure for the centrifugals.
Automation
Distribution mixers are designed for integration with an automated centrifugal station. Their operating states and feeding strategies can be included in a higher-level process control system. This supports even capacity use of the centrifugals and the downstream process steps, as well as stable and continuous operation.
Benefits
- Quick and even filling of the centrifugal(s)
- Homogeneous crystal suspensions thanks to reliable prevention of sedimentation, agglomeration and caking
- Constant operating conditions resulting in better capacity use and stable operation of the centrifugals
- Low energy consumption of the agitator and a small footprint
Model sizes / variants / customisation
Distribution mixers from BMA have a standard diameter of 1,000 mm and can therefore be integrated into almost any sugar factory. Their length depends on the number and width of the connected centrifugals. The S-type was developed to permit switching between two adjacent distribution mixers to feed one centrifugal. When a distribution mixer is filled from a massecuite pump, a dome ensures sufficient and constant system pressure for the centrifugals.